In the semiconductor industry, getting a chip to market is about more than designing a high-performance device or manufacturing it at scale. You also need to verify that it performs as intended, meets its specifications and remains reliable under real-world operating conditions.
That makes your testing infrastructure a critical part of your business strategy. Whether you manufacture integrated circuits, develop advanced chips, provide semiconductor testing services or are just planning to step into the semiconductor market, your ability to test devices efficiently can influence product development timelines, manufacturing yields and customer confidence.
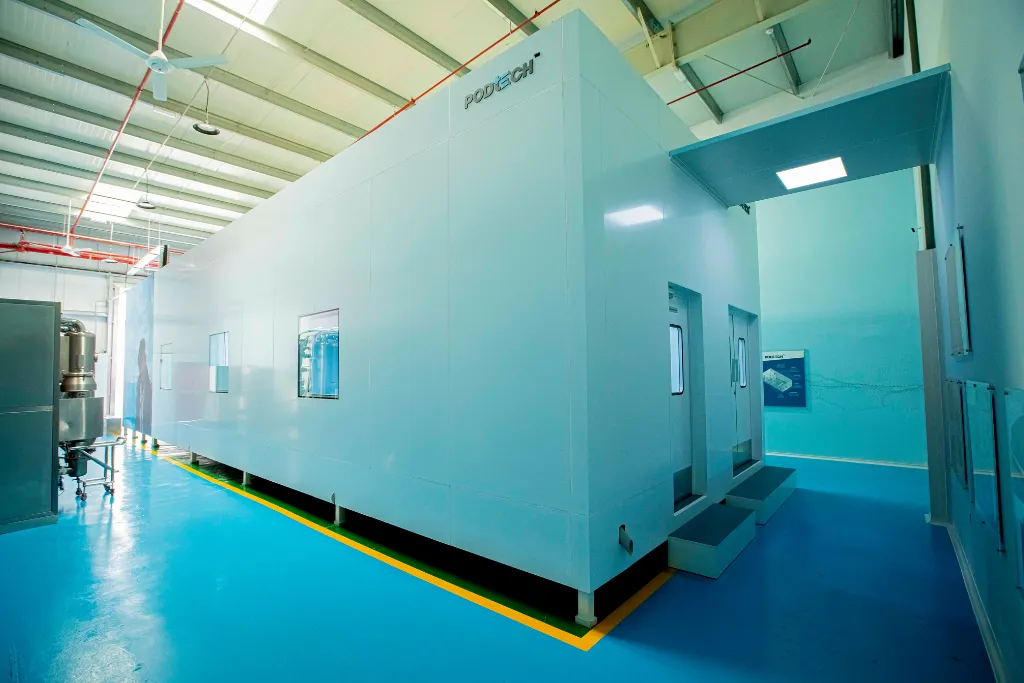
However, setting up an advanced semiconductor test lab is a complex undertaking. You need specialised equipment, precise environmental controls, reliable utilities and a facility designed around your testing requirements. Traditional construction can make this process particularly time-consuming, especially when you need to coordinate multiple contractors, integrate sensitive equipment and prepare the facility for commissioning.
A more flexible approach to facility design can help you bring testing capabilities online sooner without compromising on technical requirements.
In this guide, you will learn what an advanced semiconductor test lab does, which processes and equipment you need, and how you can plan your facility to reduce setup time and respond to a rapidly evolving market.
Understanding your semiconductor test lab requirements.
Let’s address some of the most basic questions that come up as we work with customers to set up semiconductor testing labs.
1. What is an advanced semiconductor test lab?
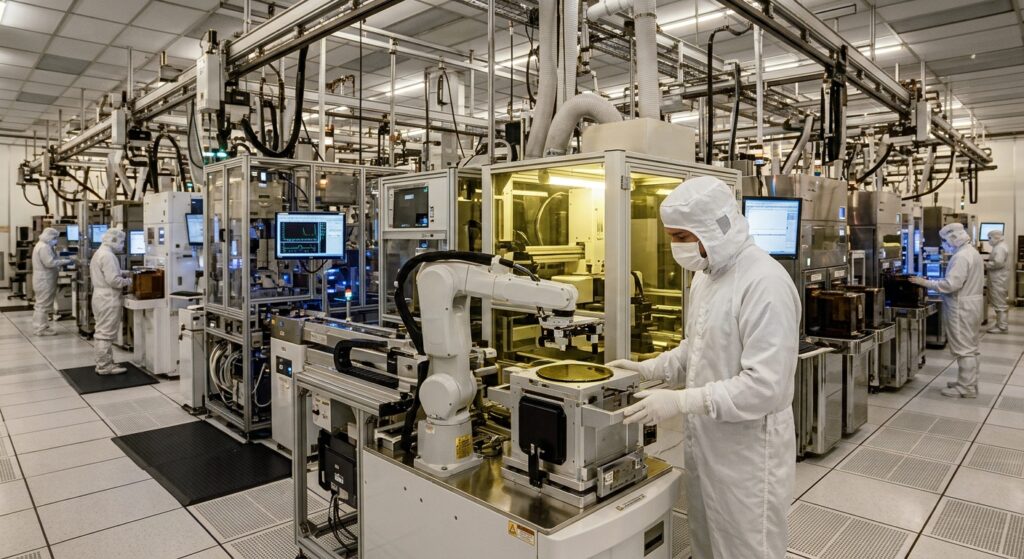
An advanced semiconductor test lab is a specialised facility where you evaluate semiconductor devices to determine whether they meet defined electrical, functional, performance and reliability requirements.
Depending on your business model, you may use your laboratory to test wafers before they are diced, characterise newly developed chips, validate prototypes, inspect packaged integrated circuits, investigate failures or conduct reliability studies.
Your requirements will depend on the devices you handle. A laboratory testing power semiconductors will need different capabilities from one evaluating high-speed digital processors, radio-frequency (RF) components, memory devices or microelectromechanical systems (MEMS).
For example, if you develop chips for artificial intelligence (AI) accelerators or high-performance computing, you may need to evaluate high-speed interfaces, power consumption, thermal behaviour and performance under demanding workloads. If you work with automotive semiconductors, reliability testing and operation across specified temperature ranges may be particularly important.
An advanced semiconductor test lab therefore involves much more than installing testing instruments in a room. You must integrate the equipment, environment, utilities, software and workflows needed to produce repeatable, trustworthy results.
Your facility may support several distinct activities:
- Design validation: Confirming that a new chip behaves according to its design specifications.
- Electrical characterisation: Measuring parameters such as voltage, current, leakage, capacitance and switching behaviour.
- Wafer-level testing: Evaluating individual dies while they remain on a semiconductor wafer.
- Final device testing: Checking packaged chips before they are released for further integration or sale.
- Reliability testing: Assessing how devices perform under specified electrical, thermal, mechanical or environmental stresses.
- Failure analysis: Investigating defects, unexpected behaviour and performance deviations to identify their underlying causes.
You do not necessarily need every capability from day one. Your first decision should be to define the devices you intend to test, the measurements you need to perform and the customers or internal teams your laboratory will serve.
2. Why is the semiconductor testing market growing?
Demand for semiconductor testing is closely connected to the increasing importance and complexity of chips across industries.
AI infrastructure, cloud computing, telecommunications, automotive electronics, industrial automation and advanced consumer devices all depend on increasingly sophisticated semiconductors. As chip architectures evolve, validating their performance and reliability becomes more demanding.
The market data reflects this shift. According to SEMI’s July 2026 equipment forecast, global semiconductor manufacturing equipment sales are projected to reach USD 165.9 billion in 2026, an increase of 23.2% over 2025. SEMI also projects semiconductor test equipment sales to grow by 31% in 2026, reaching approximately USD 15.3 billion. It attributes the expansion to AI-driven investment, advanced memory, high-bandwidth memory (HBM), increasingly complex device architectures and more rigorous testing requirements.
These figures refer to equipment sales rather than the entire semiconductor testing services market. Nevertheless, they indicate the scale of investment taking place in the technologies that support semiconductor production and validation.
Three developments are particularly relevant when you plan your facility:
Increasing chip complexity.
Advanced processors, chiplets and high-bandwidth memory introduce more demanding test requirements. You may need to evaluate multiple interfaces, high-speed signals, power delivery and thermal performance within a single testing workflow.
Greater emphasis on reliability and quality.
As semiconductors become more important to safety-critical and high-value applications, you need robust test procedures and dependable measurement systems. Detecting a defect early can help you avoid the cost of carrying it into packaging, integration or deployment.
Expanding semiconductor manufacturing capacity.
As manufacturers invest in new production facilities and regional supply chains, the need for supporting capabilities also grows. Depending on your location and business model, this can create opportunities to offer outsourced testing, design validation, characterisation or specialised reliability services.
For your business, the opportunity is not simply to establish a semiconductor laboratory. It is to establish the right capabilities at the right time, with sufficient flexibility to accommodate future technologies and customer requirements.
3. What processes are involved in semiconductor testing?
Your semiconductor testing workflow will depend on the device type, development stage, test specifications and intended application. However, most advanced testing operations involve a combination of the following processes.
Electrical characterisation.
Electrical characterisation helps you understand how a semiconductor device behaves across defined operating conditions. You measure parameters such as current-voltage characteristics, leakage current, capacitance, threshold voltage, switching performance and other device-specific metrics.
This work is particularly important during research and development, where you need to establish whether a prototype meets its design targets and understand how its behaviour changes under different conditions.
Your setup may require precision source-measure units, parameter analysers, LCR meters, waveform generators and specialised probes.
Wafer probing and wafer-level testing.
During wafer-level testing, you evaluate individual dies before the wafer is separated into individual chips. A wafer prober positions the wafer while microscopic probes establish electrical contact with selected test points.
Automated test equipment (ATE) can then execute programmed test sequences and record the results. Depending on your application, wafer-level testing may help you identify defective dies before committing additional resources to packaging.
Your wafer-probing setup must match the wafer dimensions, device geometry, probe-card requirements, temperature range and measurement precision you need.
Functional and parametric testing.
Functional testing checks whether a device performs its intended operations. For example, you may test whether a digital chip executes specified logic functions or whether a memory device reads and writes data correctly.
Parametric testing measures electrical characteristics against predefined limits. Depending on the device, these checks may include leakage, timing, drive strength, power consumption and signal integrity.
Together, these tests help you distinguish devices that meet their specifications from those that require further investigation or rejection.
RF and high-speed testing.
If you work with wireless communication chips, high-frequency components or high-speed digital interfaces, you may need specialised RF and signal-integrity testing capabilities.
Depending on your requirements, your laboratory may use vector network analysers, spectrum analysers, oscilloscopes, signal generators and dedicated RF test fixtures.
At these frequencies and data rates, the test setup itself can influence your results. Cable losses, impedance mismatches, electromagnetic interference, grounding and calibration must therefore be managed carefully.
Thermal and reliability testing.
Semiconductor devices do not always behave identically across their operating temperature range. Thermal characterisation helps you evaluate changes in performance, leakage, timing and power consumption as temperatures vary.
Reliability testing may also involve burn-in, thermal cycling, humidity exposure or other controlled stresses appropriate to your device and qualification requirements.
You should define these tests according to the relevant product specifications and industry standards. Not every laboratory needs environmental chambers or burn-in systems and the appropriate equipment will depend on the devices and qualification activities you support.
Failure analysis and reporting.
When a device fails a test, you need to determine whether the problem originates in the device, the manufacturing process, the package or the measurement setup.
Depending on the complexity of your operation, failure analysis may involve optical microscopy, curve tracing, specialised electrical measurements and advanced physical-analysis techniques available in-house or through external laboratories.
Your testing software should also support data collection, traceability, analysis and reporting. Consistent records help you compare results across devices and batches, identify recurring failure patterns and communicate findings to customers or design teams.
The key is to design your semiconductor testing facility around an end-to-end workflow rather than selecting individual instruments in isolation. Stay tuned for more in part 2!